Welding cost per meter is the number that turns a drawing into a price you can quote. Say you have 12 m of 6 mm fillet welds on a steel frame, and the customer wants a figure today. This guide walks through one clear method, with every step worked out, so you can repeat it with your own rates.
The short version: in the example below, the wire is a small part of the bill and the clock is the big part.
Quick answer
Welding cost per meter = (filler metal + shielding gas + labor + overhead) ÷ weld length. In the example below, a 6 mm fillet works out to about $8.73 per meter, and roughly three-quarters of that is labor. The rates are example numbers, so swap in your own.
Last reviewed: October 2026
The Job We Are Going to Price
Here is the job. All the rates are made-up example values, chosen to keep the arithmetic easy to follow. They are not market prices, so replace them with figures from your own shop.
| Input | Example value |
|---|---|
| Weld | 6 mm equal-leg fillet, 12 m in total |
| Process | MIG with solid wire, 93% deposition efficiency |
| Material | Mild steel, 7,850 kg/m³ |
| Filler wire price | $4.00 per kg |
| Travel speed | 300 mm/min |
| Shielding gas | 15 L/min at $0.01 per litre |
| Labor rate | $35 per hour |
| Operating factor | 30% (explained in step 3) |
| Overhead | 15% on top |
Step 1: How Much Filler Metal Does the Weld Need?
Start with the size of the weld. TWI explains that the cross-section of an equal-leg fillet weld is half the square of the leg length, and that weight is volume multiplied by density. You can read the method in TWI's guide to calculating weld volume and weight.
Filler needed = weld metal weight ÷ deposition efficiency
For our job:
- Cross-section: 0.5 × 6 × 6 = 18 mm²
- Volume: 18 mm² × 12,000 mm = 216,000 mm³, which is 216 cm³
- Weld metal: 216 cm³ × 7.85 g/cm³ = about 1.70 kg
- Filler to buy: 1.70 ÷ 0.93 = about 1.82 kg, because not all of the wire ends up in the weld
- Filler cost: 1.82 kg × $4.00 = $7.29
One honest limit: this treats the weld as a perfect triangle. TWI notes that real welds can carry excess metal on the face, so treat the result as a solid baseline rather than an exact figure.
Step 2: How Long Is the Arc On, and What Does the Gas Cost?
Arc time is simply weld length divided by travel speed.
- Arc time: 12,000 mm ÷ 300 mm/min = 40 minutes
- Gas used: 40 min × 15 L/min = 600 litres
- Gas cost: 600 L × $0.01 = $6.00
Step 3: From Arc Time to Real Job Time
Forty minutes of arc time does not mean forty minutes of work. Real jobs also include setup, positioning and handling. The share of the job time that the arc is actually burning is called the operating factor.
TWI calls the same idea the duty cycle of the welding job (not to be confused with the duty cycle rating of a welding machine). Its published typical values for workshop welding are in this table.
| Process | Typical | Range |
|---|---|---|
| Manual metal arc (stick), manual | about 25% | 15 to 40% |
| MIG/MAG, semi-automatic | about 45% | 15 to 60% |
| Flux-cored, semi-automatic | about 40% | 15 to 55% |
| MIG/MAG, automatic | about 90% | 50 to 100% |
Another trade article puts the industry average at around 20%, or about 12 minutes of arc time in every hour. The numbers differ because shops, joints and jobs differ. We will use 30% as a middle value that sits inside these ranges.
- Total job time: 40 min ÷ 0.30 = 133.3 minutes, or 2.22 hours
- Labor cost: 2.22 h × $35 = $77.78
Step 4: Add Overhead and Get the Welding Cost per Meter
| Cost line | Amount |
|---|---|
| Filler metal | $7.29 |
| Shielding gas | $6.00 |
| Labor | $77.78 |
| Subtotal | $91.07 |
| Overhead (15%) | $13.66 |
| Total for 12 m | $104.73 |
| Welding cost per meter | $8.73 |
Need it per foot instead? Multiply by 0.3048, since one foot is exactly 0.3048 m. That gives about $2.66 per foot. (The conversion factor is listed in NIST's conversion tables.)
Where the $104.73 goes in the example job
Labor 74.3% Overhead 13.0% Filler 7.0% Gas 5.7%
That is in line with what two welding writers report. A Miller Electric engineer writing in Fabricating & Metalworking puts labor at 60 to 85 percent of total welding cost. A separate article in The Welder says labor and overhead make up the largest part of the cost and that gas has a very small effect. Links to both are in the sources below.
Three Things That Move the Price Most
1. The operating factor you assume
Same weld, same wire, same wage. Only the operating factor changes.
| Operating factor | Job time | Labor | Total for 12 m | Per meter |
|---|---|---|---|---|
| 20% | 200 min | $116.67 | $149.45 | $12.45 |
| 30% | 133 min | $77.78 | $104.73 | $8.73 |
| 45% | 89 min | $51.85 | $74.92 | $6.24 |
Moving from 45% to 20% roughly doubles the cost per meter in this example. This is why it pays to use your own shop's time records instead of a textbook figure.
2. The weld size
Because the area depends on the leg squared, a slightly bigger weld needs much more metal. Going from a 4 mm leg to a 6 mm leg is 2.25 times the weld metal, not 1.5 times.
| Leg size | Weld metal per meter | Filler per meter (93%) | Compared with 6 mm |
|---|---|---|---|
| 4 mm | 0.063 kg | 0.068 kg | 0.44× |
| 5 mm | 0.098 kg | 0.106 kg | 0.69× |
| 6 mm | 0.141 kg | 0.152 kg | 1.00× |
| 8 mm | 0.251 kg | 0.270 kg | 1.78× |
| 10 mm | 0.392 kg | 0.422 kg | 2.78× |
This table counts weld metal only, not welding time.
3. The process you weld with
Deposition efficiency is the weld metal deposited divided by the filler metal consumed. Writers David Meyer and Rob Koltz give these typical figures in The Welder. The last column is simple arithmetic: how much filler you must buy for each 1 kg of weld metal.
| Process | Deposition efficiency | Filler needed per 1 kg of weld metal |
|---|---|---|
| TIG (GTAW), when filler metal is used | about 99% | about 1.01 kg |
| MIG, solid and metal-cored wire (GMAW) | 92 to 98% | 1.02 to 1.09 kg |
| Flux-cored (FCAW) | about 87% | about 1.15 kg |
| Stick (SMAW) | about 65% | about 1.54 kg |
Stick welding needs the most filler for each kilogram of weld metal. The duty-cycle table in step 3 also shows that the operating factor differs by process, so compare whole-job cost, not wire cost alone.
A Quote Sheet You Can Copy
| Line | How to work it out | Your number |
|---|---|---|
| Weld metal (kg) | 0.5 × leg² × length × density | |
| Filler needed (kg) | Weld metal ÷ deposition efficiency | |
| Filler cost | Filler kg × price per kg | |
| Arc time (min) | Length ÷ travel speed | |
| Gas cost | Arc time × flow rate × price per litre | |
| Job time | Arc time ÷ operating factor | |
| Labor cost | Job time in hours × hourly rate | |
| Overhead | Subtotal × overhead % | |
| Welding cost per meter | Total ÷ length in meters |
Before You Send the Quote
- Use the leg size on the drawing. Do not assume it.
- Price each weld size separately. If a job has 5 mm and 8 mm welds, calculate each one and add them up.
- Take the operating factor from your own records. It is the single number that changes the answer most.
- Add preparation work that the formula leaves out. Grinding and preparation are not part of this formula. The Fabricating & Metalworking article describes them as a significant labor cost in one real example.
- Keep units consistent. Millimeters with meters, kilograms with price per kg.
Where This Method Stops Working
The method above is built for single-size fillet welds. Groove (butt) welds have a different cross-section, and TWI's guide shows how to work out the area for a V-groove joint. TWI also notes that typical arc-on figures vary with the type of work, joint access and working practices, so a job that differs from your usual work may need a different operating factor. For code-critical or high-value work, ask a qualified welding engineer or estimator to review the figures.
Questions People Ask About Welding Cost per Meter
How do you calculate welding cost per meter?
Add up the filler metal, shielding gas, labor and overhead for the job, then divide by the total weld length in meters. The four steps above show how to get each of those lines.
What is a normal welding cost per meter?
There is no single normal figure, because weld size, process, labor rate and operating factor all change it. The $8.73 in this guide comes from example rates only. Use your own numbers for any real quote.
What is the operating factor in welding?
It is the percentage of total job time that the arc is actually burning. The rest goes to setup, positioning and handling. TWI describes this as the duty cycle of the welding job and lists typical values by process.
Why does a bigger weld cost so much more?
The cross-section of a fillet weld grows with the square of the leg length. A 6 mm leg holds 2.25 times the metal of a 4 mm leg.
Is labor really the biggest part of welding cost?
In the example it is 74.3% of the total. A Miller Electric engineer writing in Fabricating & Metalworking gives a range of 60 to 85 percent of total welding cost. Your own share will depend on your wire price, wage and operating factor.
How do I convert cost per meter to cost per foot?
Multiply the cost per meter by 0.3048. For example, $8.73 per meter is about $2.66 per foot.
Summary
To find welding cost per meter, work out the filler metal from the weld size, get the arc time from the travel speed, stretch it to real job time with the operating factor, then add gas and overhead and divide by the length. In the example, the wire is the small part, and the operating factor and labor rate drive the price.
This guide is for general information and estimating. The rates in the examples are illustrative, not market prices, and real jobs vary with weld shape, position, equipment, shop practice and the welder's technique. It is not a substitute for a welding procedure specification, the requirements of a code or contract, or the judgment of a qualified estimator or welding engineer. Please check your own figures before you quote or buy materials. Links to other websites are provided for reference only, and BytePriva is not responsible for their content. Read our full disclaimer.
Sources and Further Reading
- TWI: Calculating Weld Volume and Weight. Fillet weld cross-section, weight formula and steel densities.
- TWI: What typical duty cycles are achieved when arc welding? Typical arc-on percentages by process.
- The Welder (The Fabricator): Understanding the relationship between deposition rate, deposition efficiency and production output. Deposition efficiency by process and the industry-average operating factor.
- Fabricating & Metalworking: Understanding and lowering weld costs. Labor as a share of total welding cost.
- The Welder (The Fabricator): Analyze your arc welding cost. Labor, overhead and gas in the cost picture.
- NIST Guide to the SI, Appendix B.8. Exact foot-to-meter conversion factor.
Try It With Your Own Numbers
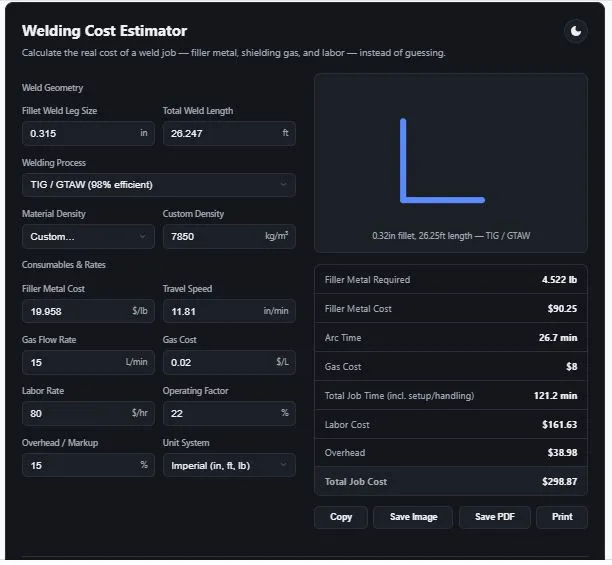
BytePriva's Welding Cost Estimator lists the same formulas for weld metal, filler, arc time, job time and labor that are used in steps 1 to 3. Its inputs are the fillet leg size, weld length, welding process, material density, filler metal cost, travel speed, gas flow rate, gas cost, labor rate, operating factor and overhead, with a metric or imperial option. It shows the filler required, filler cost, arc time, gas cost, total job time, labor cost, overhead and total job cost. Divide the total by your weld length to get the welding cost per meter. Enter your own rates, because the example rates in this guide are only illustrations.
Tool link: https://bytepriva.com/welding-cost-estimator/